Conveying & Elevating Equipment
TH‑type chain bucket elevator
The TH chain bucket elevator uses forged ring chains and fixed buckets for vertical conveying of powder, granules and small lumps.
Request a Configuration Review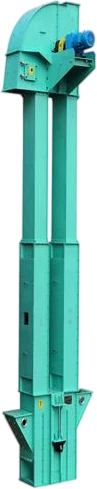
Final configuration, capacity, dimensions and price are confirmed after evaluating your material and process requirements.
Product introduction
The TH chain bucket elevator uses forged ring chains and fixed buckets for vertical conveying of powder, granules and small lumps. It is designed for robust service and higher temperature or more abrasive duties than a belt elevator.
Working principle
The head sprocket drives the ring-chain loop and attached buckets. Material enters the buckets at the boot, travels upward inside the casing and discharges by gravity at the head; tensioning components maintain chain engagement.
Product advantages
- Double-chain traction provides high load capacity.
- Ring-chain construction resists impact and elevated temperatures.
- Suitable for continuous conveying of moderately abrasive products.
- Enclosed casing and service panels support dust control and maintenance.
Suitable industries and materials
Used for ore, limestone, cement clinker, coal, fertilizers and similar bulk solids in mining, building-material, chemical, metallurgical and power plants.